 GLORY MACHINERY | Metal Polishing & Grinding Solutions
If rolling is the step that shapes a coil and polishing is the step that finishes its surface, annealing is the step that gives the coil back its ability to be formed. Without it, much cold-rolled stainless steel would simply be too hard and too brittle for the bending, deep drawing and fabrication its buyers need.
Cold rolling hardens steel. Each pass through the mill reduces thickness and raises strength, but it also reduces ductility — the material’s ability to deform without cracking. That trade-off is managed by annealing: heating the coil to a recrystallisation temperature, holding it there so the deformed grain structure reforms, and then cooling it under controlled conditions. Process descriptions of cold-rolled strip production consistently list annealing as a crucial step, needed before cold rolling, between passes, and as a final treatment, with the exact cycle varying by grade.
Where the furnace sits in the chain matters as much as what it does. In the classic route, a coil is annealed and then pickled: the heat treatment restores formability, and pickling removes the oxide scale that forms when steel is heated in air. A well-known industry sequence describes cold rolled annealed pickled (CRAP) material as hot-rolled annealed pickled coil that is cold rolled, annealed again to restore ductility, and pickled a final time for a clean, uniform surface. Annealing and surface treatment are therefore partners, not alternatives — one fixes the inside of the metal, the other fixes the outside.
There is also a second, increasingly discussed route: bright annealing. Here the coil is annealed in a controlled-atmosphere furnace, typically under a hydrogen-nitrogen mixture, so that no oxygen reaches the surface and no heavy scale forms in the first place. Industry finish guides describe bright annealed (BA) stainless as heat-treated in a controlled atmosphere furnace, giving a mirror-like appearance that may still show some cloudiness or imperfections. Because no pickling acid touches the strip, the BA surface keeps the fine texture left by cold rolling — which is exactly why surface preparation before the furnace matters. A bright anneal can preserve a good surface, but it cannot create one: dirt, rolling oil or scale carried into the furnace will still show up on the finished coil, which is why strip is cleaned before bright annealing.

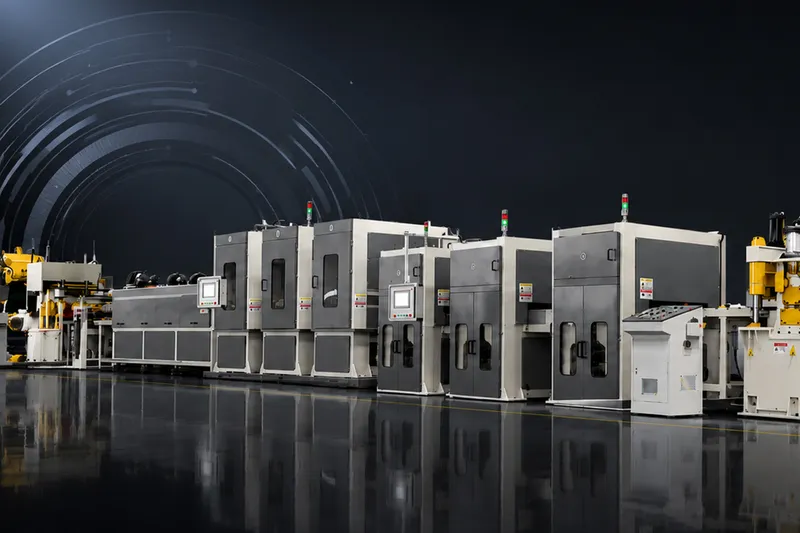
Decoiler and loading car
This is the logic of the full chain: rolling mill, then polishing, then annealing furnace. Rolling sets dimensions and strength. A coil-to-coil polishing line in the middle removes scale and surface defects and sets a uniform finish. Annealing then restores ductility and prepares the coil for forming — and, in the bright-annealing route, locks in the surface quality that polishing created. For titanium coil the same thinking applies in a different form: oxide must be removed, by mechanical grinding or chemical means, before further heat treatment and processing, because an oxide film left on the surface harms every step that follows.
Buyers comparing suppliers can use this chain as a checklist. Ask what surface condition the coil will have when it enters the furnace, what finish it should have when it leaves, and whether the line between rolling and annealing is equipped to deliver that finish consistently across the full coil width. A chain with a weak middle step will show it at the end, whatever the furnace does.
GLORY MACHINERY supplies coil-to-coil polishing lines that sit between rolling and annealing in stainless steel and titanium coil processing. Contact us for details on matching a line to your coil width and target finish.
WeChat
Scan the QR Code with WeChat